
Views: 0 Author: Zisheng Electric Technical Engineer Publish Time: 2026-10-10 Origin: Site


Zisheng Electric treats transformer core grounding acceptance as a defined design-and-test interface, not as a final continuity check performed after the tank is closed. A power-transformer core normally requires an intentional earth connection, while unintended additional conductive paths can create circulating current, local heating and misleading condition-monitoring results. For procurement teams, the practical question is therefore not simply whether the core is grounded. It is whether the complete grounding arrangement is identifiable, accessible, documented and proven against the approved design.
This guide is written for EPC engineers, transformer purchasers, factory inspectors and project owners preparing a technical specification or factory acceptance plan. It does not prescribe a universal resistance limit or an energized test method. The transformer manufacturer and responsible project engineer must define the applicable acceptance values, safety controls and test procedure for the offered design.
The review should begin with a drawing that identifies every intentional connection from the magnetic circuit to the external grounding point. Ask the supplier to distinguish the main core, clamps, frame, electrostatic shields and any structural parts that may have their own bonding requirements. A single line on a general arrangement drawing is rarely enough to explain which internal component is connected, where the conductor is routed and how the connection can be isolated for measurement.
Record the drawing revision used for production. If the grounding lead route or terminal arrangement changes after approval, the supplier should evaluate the impact on insulation clearances, mechanical support, accessibility and test interpretation. The change belongs in the same controlled design record as other internal transformer interfaces.
Require a clear component-to-terminal trace. The record should show the attachment at the core or clamping structure, the insulated lead route, the feedthrough or test link, and the external connection to the tank grounding system. Each point should have a stable identification that matches the wiring diagram, terminal schedule, inspection checklist and physical labels.
The words “single-point grounding” describe the intended electrical condition, but they do not prove that condition exists after assembly. Metal contact can be introduced by a misplaced washer, damaged insulation, debris, a lead touching structural steel or an unreviewed bracket. Acceptance therefore combines visual control during manufacture with electrical evidence at appropriate stages.
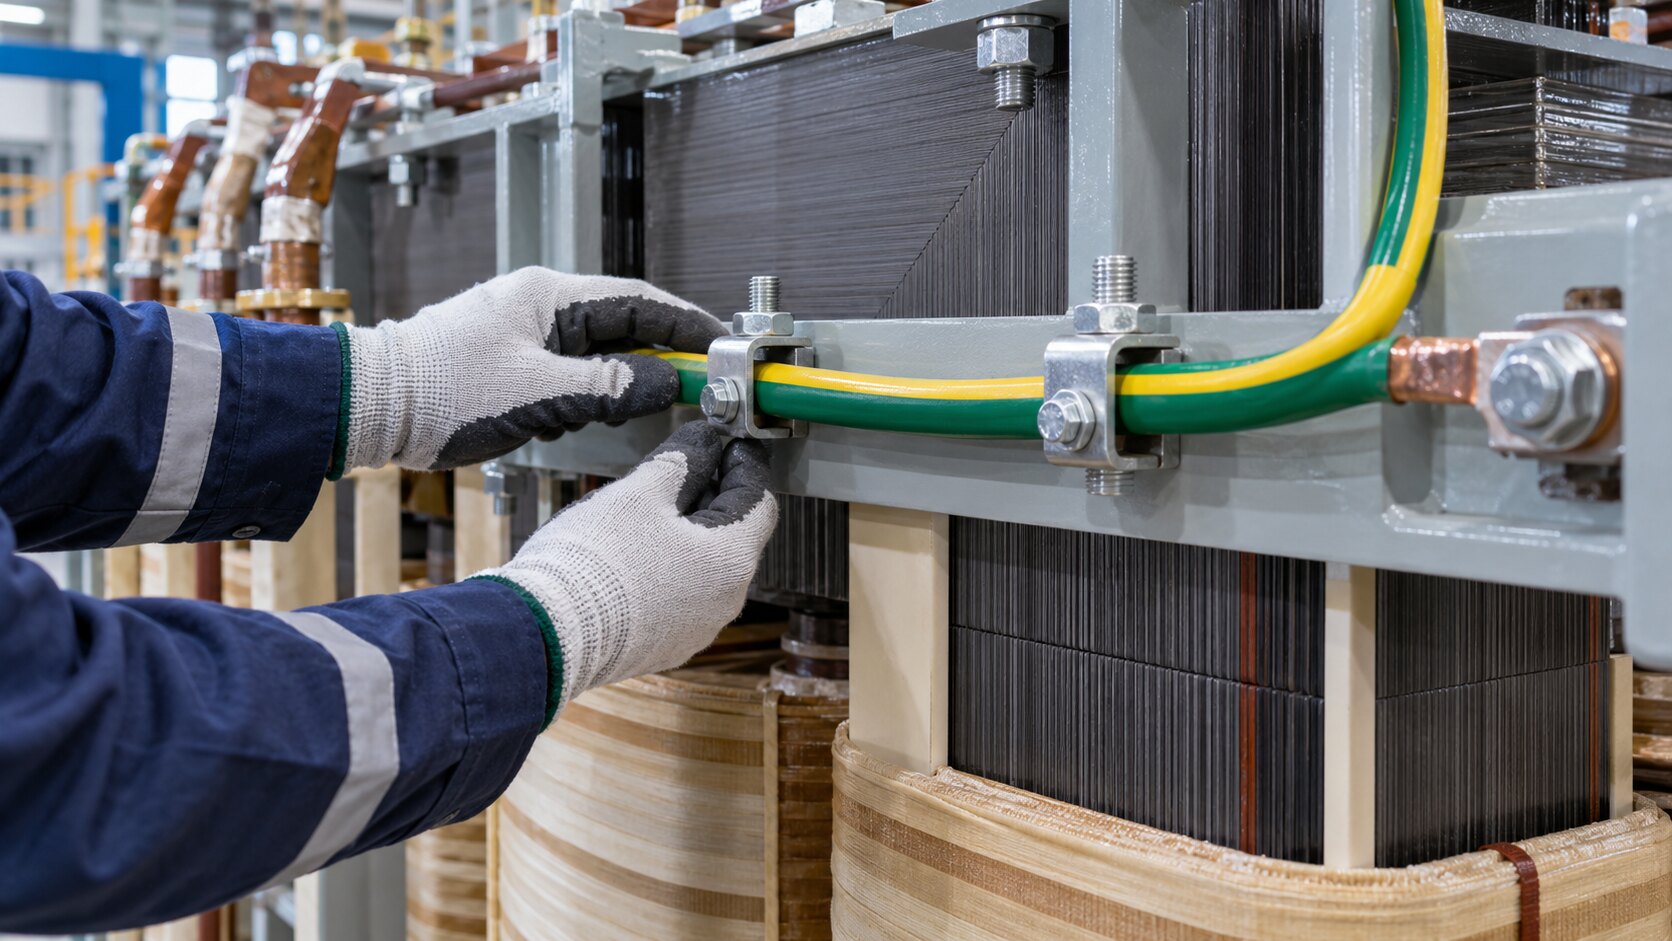
Inspect the intentional core-earth lead route and insulated interfaces while the active part remains accessible.
Procurement documents should avoid treating the core and all supporting steel as one undefined item. Depending on the design, the core, upper and lower clamps, frame components or magnetic shields may need different bonding or insulation arrangements. Ask the supplier to state the function of each connection and whether it is intentionally bonded, intentionally insulated or connected through a removable link.
This distinction matters during diagnosis. If a future measurement changes, maintenance personnel need to know which part of the magnetic assembly the external point represents. A label such as “CORE EARTH” is useful only when the as-built drawing confirms the internal boundary behind that label.
Review the details around bolts, sleeves, washers, pressure plates and support members that cross an insulation boundary. The design should prevent ordinary assembly tolerances from creating a second conductive path. Inspection records should identify critical insulating parts and show that the released material and assembly method were used.
Where the design relies on clearance from the tank or internal steelwork, confirm that transport restraint, winding movement allowances and final assembly operations do not compromise the clearance. A geometry that looks acceptable before the active part is lowered into the tank may require another check after final positioning.
A strong inspection plan collects evidence while the relevant interface is still visible. Waiting until the finished transformer reaches FAT can leave the team with a numerical result but no way to determine the location of an abnormal path. Agree the hold points, witness points and document records before production starts.
Stage |
Evidence to review |
Decision question |
Typical unresolved risk |
|---|---|---|---|
Design release |
Core and clamp grounding drawing, terminal schedule, insulation details |
Are all intentional and insulated interfaces defined? |
Generic earth symbol with no traceable internal boundary |
Active-part assembly |
Visual inspection, critical insulating components, lead routing |
Does the physical arrangement match the released design? |
Hardware bridges an insulated interface |
Before tanking |
Accessible electrical checks and photographic record |
Is the intended path present without an additional path? |
Unexplained result accepted because the assembly is about to close |
After tanking |
External terminal identity, test-link operation, repeat measurement |
Did final assembly introduce a changed condition? |
Lead contact or feedthrough damage remains hidden |
FAT release |
Final readings, calibrated instruments, drawings and deviation closure |
Can the buyer reproduce and interpret the baseline? |
Single value recorded without configuration or method |
Photographs should show context as well as detail. A close view of a lug may confirm workmanship, while a wider view shows the route and nearby structural interfaces. Use component identifiers and inspection references rather than relying on an unlabelled image folder. Photographs support the acceptance record; they do not replace drawings or required measurements.
If an external removable link is provided, review its location, labelling, enclosure and safe access. The link should allow the approved diagnostic measurement without disturbing unrelated wiring or exposing the connection to accidental damage. Its normal operating position should be unmistakable, and the handover package should explain the restoration check after any maintenance measurement.
Check the conductor and terminal materials, mechanical support and environmental protection. Outdoor terminal boxes can experience condensation, dust and corrosion, while an internal marshalling enclosure may place the connection near control wiring. The arrangement should suit the actual enclosure and service conditions rather than copy a standard detail without an interface review.
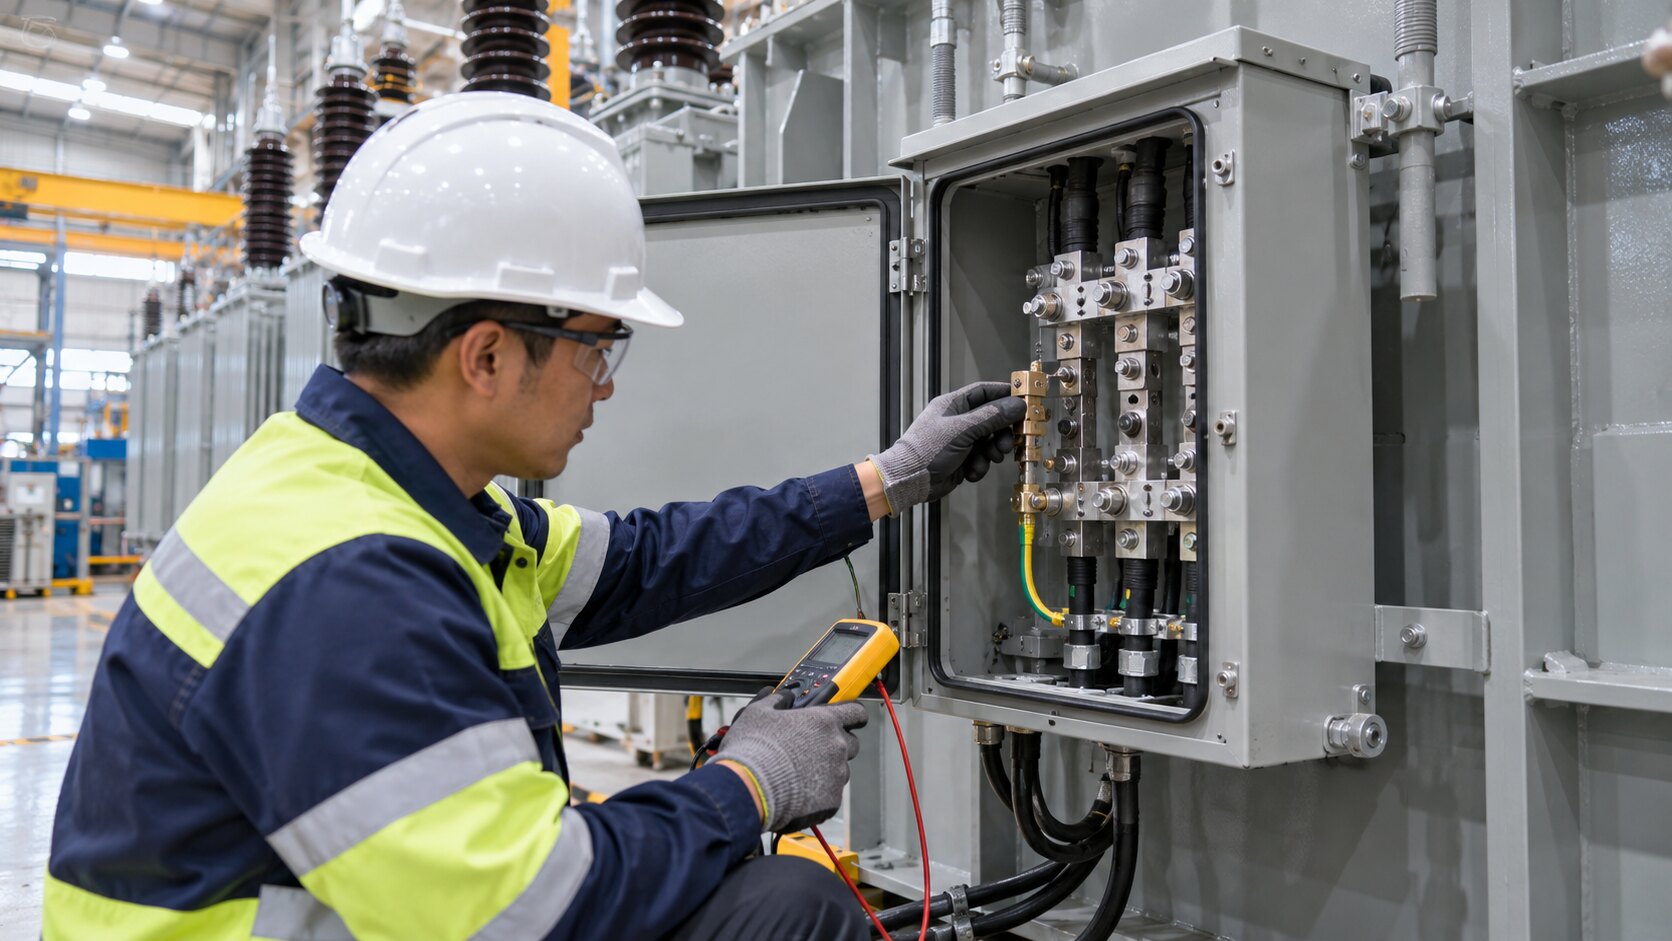
Confirm the removable test link, terminal identity and restoration arrangement before factory release.
The core grounding point should not be confused with the main tank earth pads, neutral earthing connection or instrument cable screens. Drawings and labels should use consistent names. If a monitoring device is added to the core-earth lead, define its orientation, range, output, auxiliary supply and bypass or maintenance arrangement, and identify who approves the final circuit.
Acceptance records need the test configuration, instrument, connection points and transformer assembly state. A resistance value without this context cannot be compared reliably with a later reading. State whether other intentional bonds were connected, whether the test link was open or closed, and which parts of the active assembly were included in the measurement boundary.
Do not copy a universal acceptance number from another transformer. Construction, instrument method, moisture state and test configuration can affect readings. Require the manufacturer to propose values and interpretation for the offered unit, then obtain approval through the project’s technical process. Any unexpected result should trigger investigation and documented disposition rather than informal averaging.
Where practical, compare measurements at agreed manufacturing stages. A change after tanking or final accessory assembly can be more informative than a lone final result. The record should identify what changed between the two measurements and whether the same method and instrument configuration were used.
If a second path is suspected, fault-finding should follow an approved manufacturer procedure under safe conditions. The procurement specification should require diagnosis and evidence, not instruct site personnel to disconnect internal bonds or apply test voltages without design authority.
Review the result alongside insulation, winding, tank and accessory records. An unexplained grounding anomaly can affect release decisions even when unrelated routine-test values appear acceptable. Conversely, a satisfactory core-ground check does not replace the transformer’s other required tests. The FAT index should make these relationships visible without presenting one result as proof of the whole transformer.
The transformer nameplate data review provides a useful model for reconciling physical identification with approved documents. For internal magnetic and structural interfaces, the transformer tank stray-flux heating review shows why apparently small steelwork details should remain connected to design evidence.
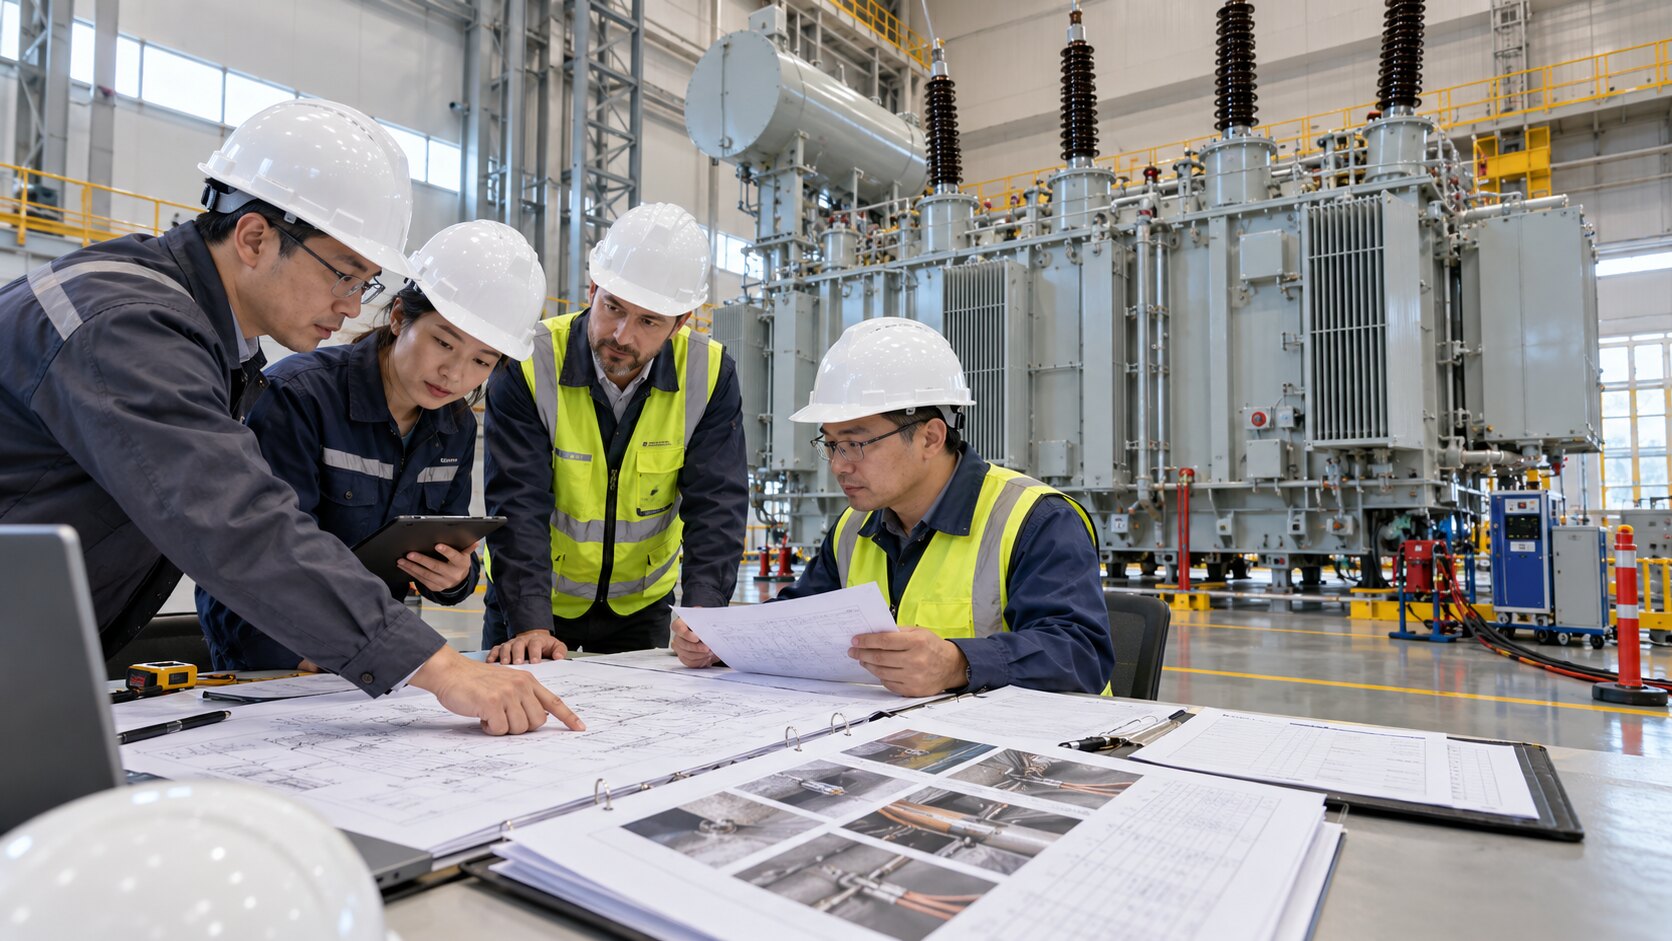
Reconcile staged measurements, drawings and inspection records into a traceable FAT evidence package.
The final dossier should include the approved grounding drawing, internal inspection evidence, measurement method, instrument identification, final readings, deviations and photographs. Record the normal position of every removable link and the labels installed on the transformer. Maintenance instructions should explain when the connection is inspected and what project authority reviews a changed result.
At site, confirm that shipping work, accessory installation and external wiring have not altered the arrangement. Where the contract requires a repeat check, compare it with the factory baseline using the approved method. A difference should be investigated with the manufacturer before energization; it should not be dismissed solely because the external lead still shows continuity.
Include document-review timing in the purchase schedule. The core-grounding drawing should be approved before the active-part inspection, and any monitoring interface should be frozen before the marshalling wiring is released. Late clarification can force the factory to reopen completed work or leave the buyer unable to witness the most useful stage. The inspection and test plan should name the records supplied before each witness point, the response period and the party authorized to accept a deviation.
Ask how the factory controls cleanliness around insulated core and clamp interfaces. Metallic swarf, loose hardware and damaged insulation can undermine an otherwise sound drawing. The answer should describe manufacturing controls and inspection evidence for the offered unit, rather than make a general statement about workshop housekeeping. Where a nonconformance is found, require the corrective action, reinspection result and affected drawing or procedure revision.
Some owners request a core-earth current monitor for large or critical transformers. Define whether the device is used for local indication, remote alarm, trending or maintenance measurements. Agree its measuring range, accuracy statement, output signal, alarm ownership, cable screening and terminal location. The monitor should not create an undocumented alternative grounding path, and its removal or bypass should leave a clearly defined safe configuration.
FAT should demonstrate the installed monitor and its signal path to the agreed boundary, while distinguishing a functional simulation from a proven service alarm threshold. Record the configuration used for the demonstration. Commissioning personnel can then reconcile the device, wiring and control-system tag without interpreting an unlabeled loop after installation.
Ask bidders to submit the core-and-clamp grounding philosophy, marked drawings, test-link details, inspection stages, proposed measurement method and acceptance criteria. Clarify whether online monitoring is required and define the interface with the control system. Include the enclosure environment, auxiliary supply, alarm contacts and document deliverables in the same enquiry.
For an oil-immersed transformer or a project-specific 110–115 kV power transformer, Zisheng Electric can develop the grounding arrangement with the active-part design and FAT plan. The transformer core grounding acceptance package should allow the buyer to trace the intended path, understand the test boundary and retain a dependable as-built baseline.
Provide drawings, data sheets, load lists, technical specifications, single-line diagrams, grid parameters, environmental conditions and installation-site conditions. Include the required grounding philosophy, monitoring interfaces, witness points and document format. Our engineering team will review the requirements and respond to project inquiries within 24 hours.


